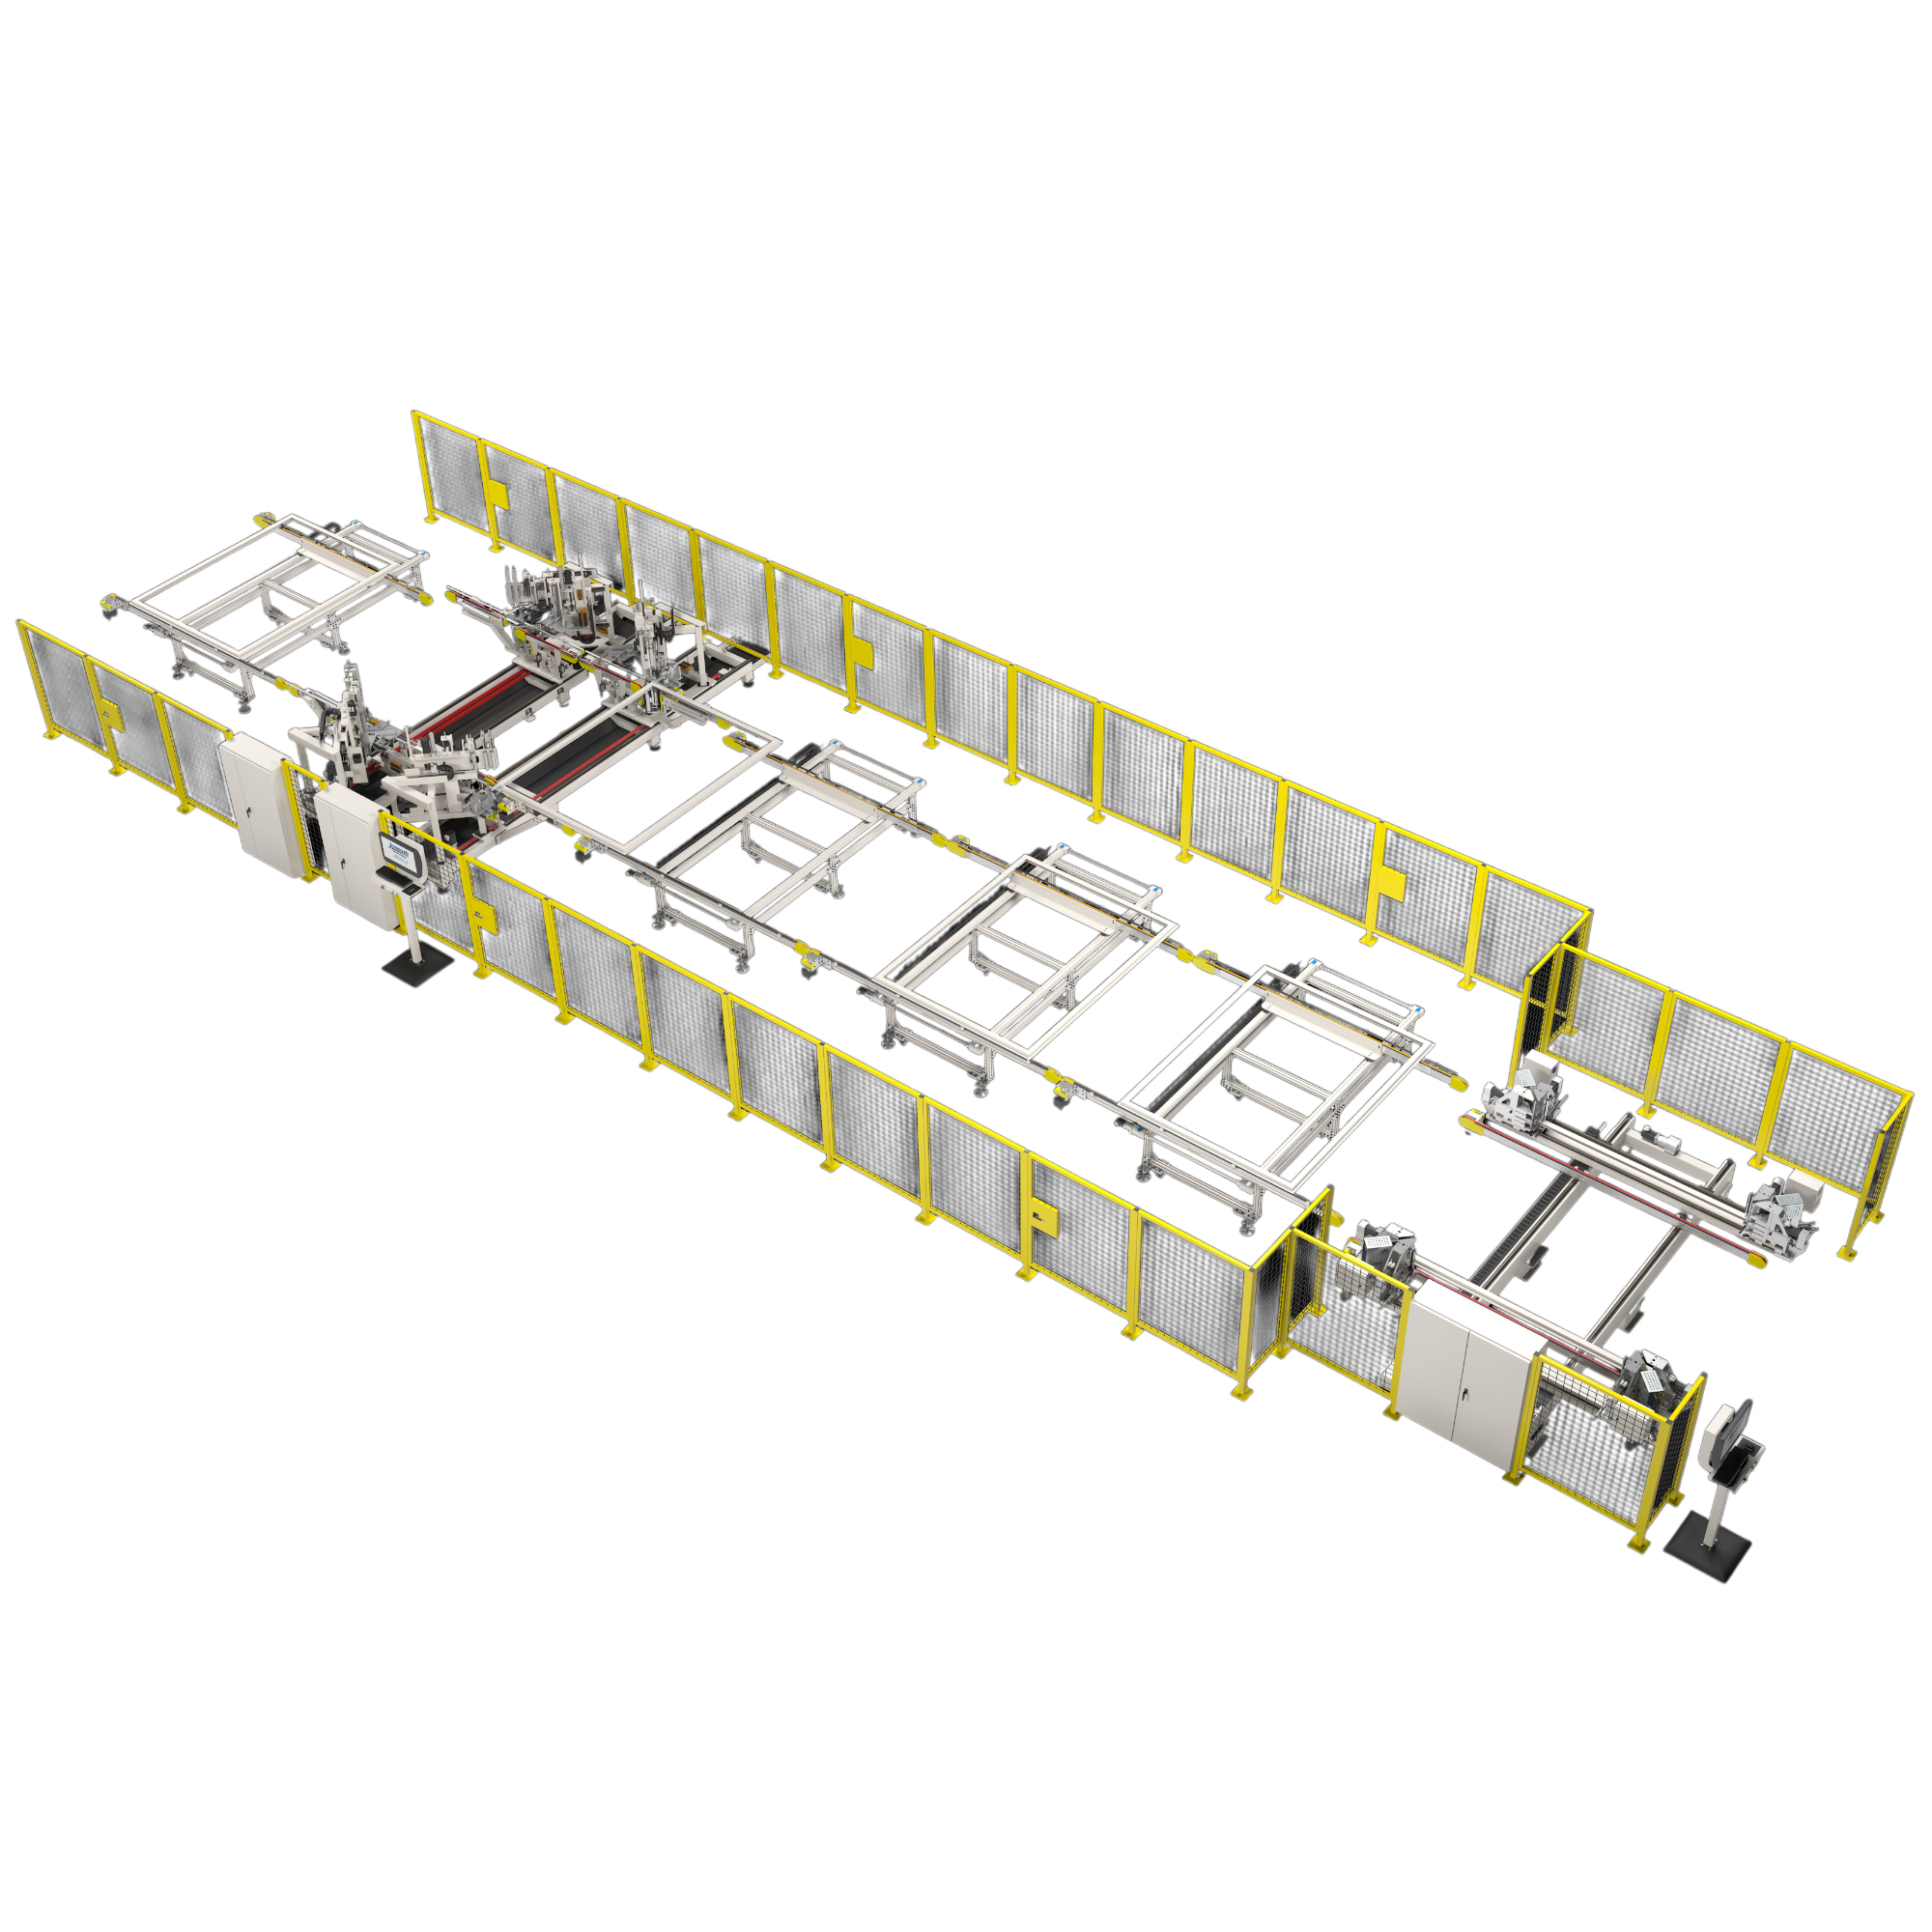
Most optimisation software runs in an office, on assumptions about what your machine does. JMCSaw runs on the saw itself, using the actual saw settings in front of it. That difference is the reason theoretical yield and real yield are not the same number.
There is no single optimisation algorithm that wins on every batch. The best cutting sequence for a batch of 50 mixed-length parts depends on the parts, the stick lengths available, and what is left over from the batch before.
So JMCSaw runs three. We developed each one separately, using a different approach, and tested all three across hundreds of batches of real customer data. Sometimes the first returns the best yield. Sometimes the third does. JMCSaw runs all three on every batch and uses whichever wins.
Against single-algorithm software, that is worth 2–3% material yield. On a line where every 1% of yield is worth $27,000 a year, that pays for itself quickly. See the full material yield cost model.
Optimisation decides the cutting order. It cannot make the last piece of every stick disappear. Two features go after what is left.
At the end of each stick, if the remaining length is usable, JMCSaw looks into upcoming batches and finds parts it can make now. Set it to Fill In and the software selects the best-fitting part automatically. Set it to Operator’s Choice and it shows the operator every part that would fit and lets them decide.
When that batch later comes up as the current batch, the operator is told which parts already exist, and those parts are locked so they are not cut twice.
The same tail-end logic pointed at stock parts. You define which parts to hold in stock, a priority order, and a maximum count. At the end of each stick JMCSaw makes those parts from material that would otherwise be scrap, up to the count you set.
It also works backwards. When a stock part already on the shelf matches something in the current batch, the operator is prompted to use it rather than cut a new one.
Both features depend on precise, repeatable positioning of material at the end of a stick, which is why they require a ProCut servo infeed pusher.
Yield is not only an algorithm problem. A blade past its service life cuts badly and produces remakes, and remakes are scrap by another name.
JMCSaw tracks cycles per tool against limits you set. It warns the operator on the fab status screen when a tool passes its PM count. If a tool passes its maximum count, the machine locks the operator out of starting another batch until maintenance resets it. Every reset is logged.
It is a deliberately blunt control. It exists because the alternative is discovering the problem in your remake numbers a week later.
When we last rebuilt the optimiser we tested it against more than 200 real customer batches, ranging from 50 to 100 records each, supplied by manufacturers already running JMCSaw. We kept the new result only where it genuinely improved on what came before.
© 2025 Joseph Machine Company. All right reserved. Privacy Policy. Sitemap.